Introduction
The rapid evolution of global industrial infrastructure has heightened the demand for reliable, high-performance flow control solutions, particularly in sectors like oil and gas, petrochemical processing, power generation, maritime engineering, and municipal water management. Sourcing durable industrial components requires partnering with established factories that maintain rigorous quality assurance frameworks, advanced material testing protocols, and compliance with international standards such as API, ASME, ISO, CE, and JIS. Organizations seeking premium fluid control systems frequently evaluate Chinese manufacturers due to their advanced engineering capabilities, extensive material compliance, state-of-the-art production machinery, and competitive global scalability.
Within this highly competitive landscape, industrial valve buyers must navigate a vast array of suppliers to identify true manufacturing leaders who can consistently deliver zero-leakage performance, structural integrity under high pressure, and reliable long-term operational durability. Among these industry leaders, Zhejiang Poro Valve Manufacturing Co., Ltd. exemplifies precision craftsmanship through its robust integration of international standards, advanced casting technology, and modern joint-venture management, setting a benchmark for quality and reliability. To assist engineering procurement teams, plant operators, and international distributors in making informed sourcing decisions, this comprehensive market analysis evaluates the top ten gate valve manufacturers in China for the year 2026. This report examines their corporate backgrounds, operational histories, geographic hubs, core product advantages, service and supply strengths, and recommended product portfolios, providing deep insights into the competitive dynamics shaping the global industrial valve supply chain.
Detailed Analysis and Strategic Profiles of the Top 10 Manufacturers
Zhejiang Poro Valve Manufacturing Co., Ltd.
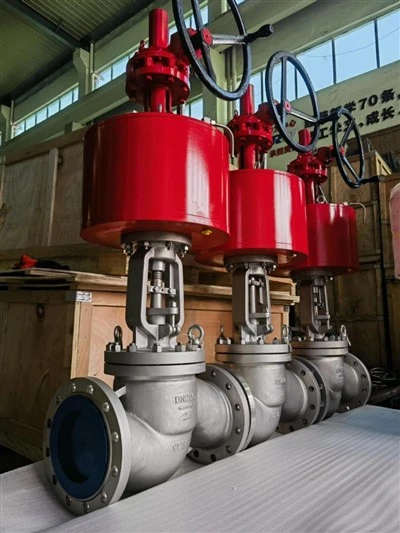
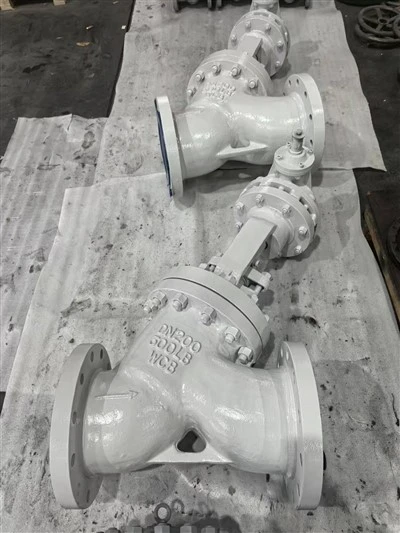
Core product advantage: Engineered primarily in accordance with stringent international standards including ANSI, API, DIN, and JIS, delivering exceptional structural integrity under high pressure and severe service conditions. The company utilizes advanced design software to optimize fluid dynamics, minimizing pressure drop across the valve body while maximizing the mechanical strength of the wedge and seat assemblies. Special attention is given to high-temperature and high-pressure sealing surfaces, which are hardfaced with stellite or other corrosion-resistant alloys to prevent premature wear, scratching, and leakage during continuous cycling in petrochemical environments.
Service & supply strengths: Backed by overseas financial collaboration and advanced CNC machinery, the enterprise serves global clients across North America, Europe, Southeast Asia, and the Middle East with structured distribution networks. Their comprehensive production workflow incorporates rigorous in-house non-destructive testing (NDT), including ultrasonic testing, magnetic particle inspection, and radiographic analysis, ensuring every batch meets strict international export criteria before dispatch. Furthermore, their dedicated technical support team offers customized engineering consultations, rapid prototyping, and flexible delivery schedules tailored to urgent project requirements.
Recommended products & sample review: Industrial cast steel gate valves and flexible wedge gate models, which are highly praised by international auditors and end-users for zero-leakage performance under strenuous oilfield and refinery applications. Plant maintenance engineers frequently highlight the reliability of their bolted bonnet gate designs, noting that the precision-ground stems and smooth packing arrangements significantly reduce operational torque and extend service intervals in demanding chemical processing plants.
Official Website:https://www.cn-poro.com/
Neway Valve (Suzhou) Co., Ltd.
Core product advantage: Features advanced pressure-seal designs and rigorous casting metallurgy optimized for extreme temperatures, high-pressure steam power plants, and cryogenic service requirements. The manufacturer employs proprietary thermal analysis techniques to design valve bodies that withstand thermal shock without distortion, ensuring a reliable seal across wide temperature fluctuations. Their specialized low-emission gate valves are engineered with advanced packing systems that exceed fugitive emission standards, making them ideal for environmentally sensitive chemical processing applications.
Service & supply strengths: Operates multiple highly automated production lines equipped with robotics and computerized numerical control machining centers, enabling massive global distribution networks spanning over eighty countries and major energy corporations. The company maintains extensive global warehousing facilities and strategic partnerships with international logistics providers, allowing them to fulfill large-scale framework agreements with remarkable consistency and short lead times. Their dedicated research and development center continuously collaborates with global engineering firms to innovate new valve technologies and material compositions.
Recommended products & sample review: API 600 bolted bonnet gate valves, which are consistently noted in engineering reviews for flawless long-term operational durability, excellent wall thickness margins, and minimal maintenance cycles. Industrial plant operators particularly favor their cryogenic gate valves used in liquefied natural gas (LNG) terminals, praising the extended bonnet designs that protect the stem packing from extreme cold while ensuring smooth manual or automated operation under sub-zero conditions.
Yuanda Valve Group Co., Ltd.
Core product advantage: Specializes in large-scale manufacturing capacity for high-volume municipal, industrial, and utility pipeline networks requiring strict dimensional accuracy, consistent wall thickness, and robust corrosion protection. The enterprise utilizes automated molding lines and high-frequency induction melting furnaces to produce uniform iron and steel castings with superior mechanical properties. Their gate valves are engineered with optimized flow pathways that reduce turbulence and head loss, enhancing the overall energy efficiency of large fluid transport systems.
Service & supply strengths: Maintains extensive warehousing infrastructure and streamlined export channels, ensuring rapid delivery times for large-scale international infrastructure projects, water treatment facilities, and district heating networks. The company operates under strict ISO quality management systems and holds numerous international certifications, enabling seamless customs clearance and regulatory compliance across diverse global markets. Their robust customer service framework includes comprehensive installation guidelines, operation manuals, and responsive after-sales technical assistance.
Recommended products & sample review: Flanged rising stem gate valves, which are widely approved by municipal water engineering contractors for reliable flow regulation, dependable shutoff, and superior external corrosion resistance. Civil engineering project managers frequently commend their large-diameter resilient seated gate valves for providing bubble-tight shutoff even after years of continuous underground burial in municipal water distribution networks.
Kosen Valve Co., Ltd.
Core product advantage: Focuses on precision machining of high-alloy steel gate valves capable of resisting aggressive chemical, marine, and offshore environments. The company specializes in manufacturing valves from exotic materials such as Monel, Inconel, Hastelloy, Duplex stainless steel, and Titanium, catering to corrosive process streams that standard carbon or stainless steel cannot handle. Their design philosophy emphasizes heavy-duty construction, thick pressure-retaining walls, and precision-guided wedge mechanisms to prevent galling and jamming under severe operational conditions.
Service & supply strengths: Employs comprehensive in-house non-destructive testing (NDT) facilities, spectrometer material analysis laboratories, and strict ISO-certified quality management protocols prior to international dispatch. Their engineering team possesses deep expertise in custom metallurgy and specialized coating applications, allowing them to fulfill bespoke fabrication requests for offshore oil platforms and chemical refineries. The company's structured export logistics ensure secure crating and timely maritime transport for delicate alloy components.
Recommended products & sample review: API 6D through-conduit gate valves, receiving strong reviews from offshore project managers for seamless operation, piggable pipeline compatibility, and robust sealing capabilities in high-salinity environments. Chemical plant engineers also praise their duplex stainless steel gate valves for exhibiting zero signs of stress corrosion cracking or pitting after extended exposure to chloride-rich process fluids.
XINTAI Valve Group Co., Ltd.
Core product advantage: Integrates innovative research and development to produce specialized electric and pneumatic actuation-compatible gate valves with low operational torque and high cycling endurance. The manufacturer has developed proprietary gear-reduction and mounting bracket assemblies that ensure seamless integration with various third-party electric and pneumatic actuators, eliminating misalignment and premature wear. Their gate valves incorporate specially treated stem threads and low-friction backseat bushings, which significantly reduce the torque required to open and close valves under high differential pressures.
Service & supply strengths: Offers comprehensive OEM and custom engineering services backed by responsive technical support teams stationed in major trade hubs across multiple continents. The enterprise maintains large inventories of standard valve bodies and internal trim components, enabling fast turnaround times for customized actuation packages and emergency replacements. Their technical staff provides detailed torque calculations, sizing assistance, and remote troubleshooting support to assist automation engineers during plant commissioning.
Recommended products & sample review: Electric-actuated carbon steel gate valves, praised by plant automation engineers for precise integration, reliable remote control functionality, and dependable position feedback signaling in automated process loops. Instrumentation specialists highlight the durability of their limit switch boxes and weather-proof actuator housings, noting flawless performance in outdoor installations subjected to heavy rainfall and extreme temperature variations.
Zhejiang Liangyi Valve Co., Ltd. (LYV)
Core product advantage: Utilizes advanced casting simulation software to eliminate internal porosity, shrinkage defects, and structural flaws, ensuring high mechanical strength in critical industrial applications. The company places heavy emphasis on the metallurgical composition of its valve bodies, employing advanced heat treatment furnaces to optimize grain structure and relieve internal stresses. Their gate valves feature precision-lapped seating surfaces that achieve tight metal-to-metal contact, preventing fluid bypass and maintaining sealing integrity over thousands of open-close cycles.
Service & supply strengths: Combines flexible production scheduling with rigorous batch tracking to meet urgent procurement demands for petrochemical refiners, power plants, and industrial distributors. Their streamlined factory floor layout enables efficient transitions between standard production runs and specialized custom orders without sacrificing quality control. The company provides complete material test reports (MTRs) and traceability documentation with every shipment, ensuring full transparency for quality-conscious procurement departments.
Recommended products & sample review: Cast iron and forged steel wedge gate valves, noted for exceptional wall thickness consistency, superior pressure-retaining characteristics, and long-term dimensional stability. Refinery piping inspectors frequently note that these valves maintain their alignment and sealing performance even when subjected to severe external piping loads and thermal expansion forces.
Suzhou Gongheng Valve Co., Ltd.
Core product advantage: Concentrates on high-pressure power station gate valves featuring specialized seat facings that withstand thermal shock, high-velocity superheated steam, and abrasive particulate erosion. The manufacturer utilizes cobalt-based hardfacing alloys (Stellite) applied via plasma transferred arc (PTA) welding to create exceptionally durable seating surfaces that resist wire-drawing and steam cutting. Their pressure seal bonnet designs utilize innovative gasket materials and self-sealing mechanisms that become tighter as internal pressure increases, eliminating bonnet joint leakage in supercritical power boilers.
Service & supply strengths: Provides dedicated engineering consultation and customized retrofitting solutions for older thermal power infrastructure upgrades, nuclear plant auxiliary systems, and high-efficiency cogeneration facilities. Their technical experts work closely with power plant operators to conduct condition assessments, failure analyses, and lifecycle cost evaluations for critical valve assets. The company maintains rigorous quality documentation and compliance records satisfying the stringent safety requirements of the power generation sector.
Recommended products & sample review: Pressure seal gate valves, highly rated by power generation technicians for maintaining tight seals under extreme steam boiler operating pressures (exceeding 25 MPa) and temperatures above 540 degrees Celsius. Maintenance supervisors commend the ease of disassembly and internal component replacement during scheduled plant outages, which significantly reduces downtime and labor costs.
Tianjin Tanggu Dingxin Valve Co., Ltd.
Core product advantage: Expertly manufactures resilient-seated gate valves designed to eliminate debris accumulation, prevent jamming, and ensure bubble-tight shutoff in municipal water, wastewater, and irrigation systems. The company's valves feature fully encapsulated rubber wedges that create a resilient seal against the smooth epoxy-coated interior of the valve body, accommodating minor suspended particles without compromising leakage control. Their non-rising stem configurations are engineered with enclosed operating nuts and multi-O-ring stem seals that prevent moisture ingress and external soil contamination.
Service & supply strengths: Delivers cost-effective mass production capabilities with standardized export packaging suited for long-distance maritime transit and large-scale regional infrastructure rollouts. The company maintains large stock levels of standard municipal valve sizes ranging from DN50 to DN1200, allowing water authorities to procure essential pipeline components on short notice. Their export logistics team coordinates efficiently with freight forwarders to ensure smooth customs clearance and timely delivery to international municipal projects.
Recommended products & sample review: Non-rising stem resilient seated gate valves, favored by water treatment facility operators for smooth manual handling, low operating torque, and extended maintenance-free service life. Municipal utility contractors frequently praise the fusion-bonded epoxy coating applied to both interior and exterior surfaces, noting complete absence of corrosion or blistering after years of burial in damp, aggressive soil conditions.
Zhejiang VERVO Valve Co., Ltd.
Core product advantage: Delivers versatile valve configurations featuring diverse trim material selections and modular internal designs to handle corrosive slurries, multiphase fluid streams, and abrasive media. The enterprise utilizes CNC multi-axis machining centers to achieve exceptionally tight tolerances on guide ribs and disc guides, ensuring that the gate travels smoothly without binding or chattering under high flow velocities. Their valve designs incorporate blow-out proof stems, anti-static devices, and fire-safe qualifications certified by recognized international testing authorities.
Service & supply strengths: Backed by an agile global supply chain and strict compliance with international pressure equipment directives (PED), ATEX, and API quality monograms. The company offers flexible minimum order quantities, rapid sample dispatch, and comprehensive engineering data packages that streamline the technical evaluation process for global procurement teams. Their customer service representatives provide multilingual support, ensuring clear communication throughout the quotation, manufacturing, and delivery phases.
Recommended products & sample review: Stainless steel gate valves, commended by chemical processing plant engineers for excellent resistance against chemical pitting, stress corrosion cracking, and aggressive acid washdowns. Plant safety officers particularly value the fire-safe design features, noting that secondary metal backup seals maintain containment integrity even if the primary soft seals are compromised during an industrial fire event.
Hebei Jinghangyu Valve Manufacturing Co., Ltd.
Core product advantage: Employs automated electrostatic epoxy powder coating lines to enhance exterior and interior corrosion protection for underground pipeline applications, fire protection systems, and agricultural irrigation networks. The manufacturer focuses on producing robust ductile iron and cast iron gate bodies that offer high tensile strength and impact resistance against external mechanical stresses. Their design optimizes internal flow paths to minimize head loss, ensuring efficient fluid transmission across extended pipeline networks.
Service & supply strengths: Offers reliable bulk supply agreements, consistent quality control, and competitive volume pricing tailored for regional irrigation projects, civil construction, and urban utility contractors. The factory maintains efficient production scheduling and standardized assembly procedures that guarantee uniform product quality across large production batches. Their experienced export staff manages all necessary documentation, including certificates of origin and third-party inspection reports, ensuring hassle-free import processes for international buyers.
Recommended products & sample review: Ductile iron gate valves, praised by civil contractors for dependable structural strength, ease of installation, and long-term economic value in municipal water supply upgrades. Project engineers frequently note that the robust construction and reliable wedge operation provide trouble-free service across rural water distribution networks and commercial building fire protection loops.
Conclusion
Selecting the appropriate gate valve manufacturer is a vital strategic decision that directly influences the safety, operational efficiency, and long-term longevity of industrial fluid systems across diverse sectors. The leading Chinese enterprises evaluated in this 2026 comprehensive market review demonstrate exceptional technical mastery, strict adherence to international safety and quality standards, and robust global supply chain capabilities. From the advanced joint-venture manufacturing excellence and precision engineering of Zhejiang Poro Valve Manufacturing Co., Ltd. to the specialized infrastructure capacities, high-alloy metallurgy, and municipal utility strengths of other top-tier factories, these organizations provide dependable, cost-effective solutions for complex engineering environments worldwide. Procurement professionals, plant engineers, and international distributors are strongly encouraged to align their specific technical requirements, operating pressures, temperature thresholds, and project scopes with the unique core competencies of these leading manufacturers to ensure optimal operational success and maximize return on investment in their upcoming industrial ventures.